Precision-engineered structural steel shelving engineered for maximum load integrity, anti-corrosive durability, and dynamic retail merchandising in Noro, Solomon Islands.
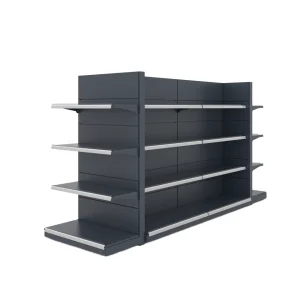
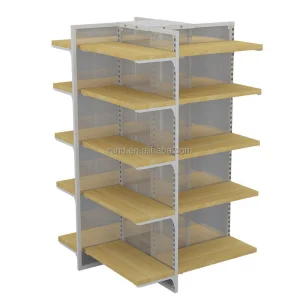
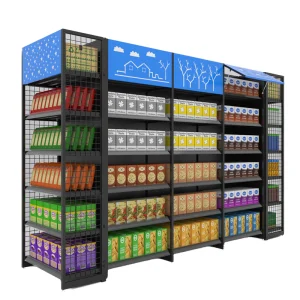
As the primary economic engine and port city of the Western Province in the Solomon Islands, Noro serves as a crucial maritime logistics junction, seafood processing hub, and FMCG wholesale redistribution center for surrounding islands including Gizo and Munda. Modern commercial retail in Noro demands racking systems capable of withstanding both extreme physical loads and harsh tropical island microclimates.
Traditional low-capacity retail fixtures routinely fail in high-humidity maritime environments like Noro due to rapid oxide formation, weld seam decay, and structural deflection under bulk canned food, liquid beverage, and commercial grain weight. Deploying certified heavy supermarket shelves engineered with high-tensile cold-rolled steel and marine-grade electrostatic powder coatings is paramount for long-term operational profitability.
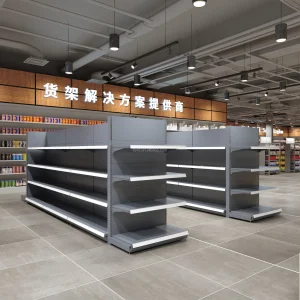
The global supermarket and grocery retail sector is experiencing a rapid convergence between retail display aesthetics and industrial warehouse durability. Modern hypermarket operators are shifting from light-duty 40kg shelves to high-density heavy-duty gondola units that serve dual purposes: customer merchandising and floor-level micro-warehousing.
Designed through structural Finite Element Analysis (FEA) to ensure failure-proof operation across demanding retail, marine hardware, and wholesale application scenarios.
Fabricated using high-grade Q235B cold-rolled structural carbon steel. Upright posts undergo continuous automated cold-roll forming to create multi-flanged geometry, dramatically elevating torsional rigidity and vertical buckling resistance compared to standard open-channel steel posts.
Shelf support brackets feature 3-hook to 4-hook precision laser-cut connector teeth that slot seamlessly into upright post perforations. Safety lock pins prevent accidental dislodgement caused by forklift bump impact or heavy manual stocking activities.
Every steel component undergoes automated 7-stage chemical pretreatment (oil removal, acid descaling, zinc phosphating, deionized water rinsing, and anti-corrosive passivation). The final exterior layer consists of non-toxic, lead-free thermosetting powder applied electrostatically at 200°C.
Bottom shelf panels are fortified with double or triple hat-channel stiffness ribs welded longitudinally underneath. This structural ribbing dissipates concentrated point loads evenly across the surface, maintaining a flat plane even under maximum capacity loads of 120kg–300kg per layer.
From waterfront wholesale trade centers to high-footfall grocery chains in Noro, our structural shelving lines adapt to diverse commercial operational realities.
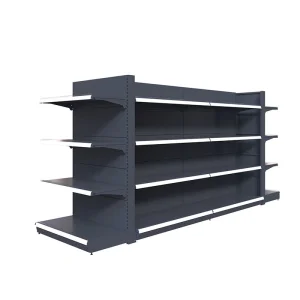
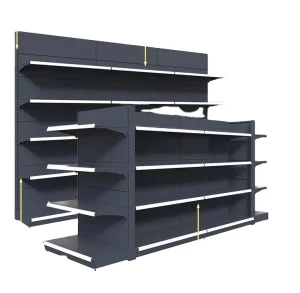
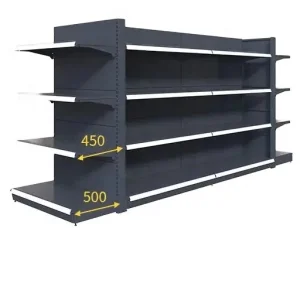
Specially engineered four-column heavy gondolas and back-net racking units built to handle palletized stock breakdown, heavy beverage crates, and bulk food staples common in island supply chain redistribution centers.
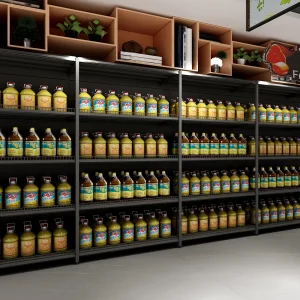
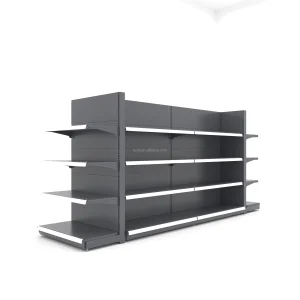
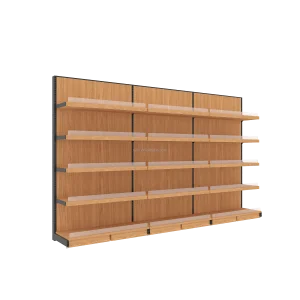
Heavy-duty double-sided steel gondolas with custom wooden or acrylic accents. Provides premium aesthetic merchandising for imported goods, personal care items, and processed seafood lines while resisting salty tropical air.
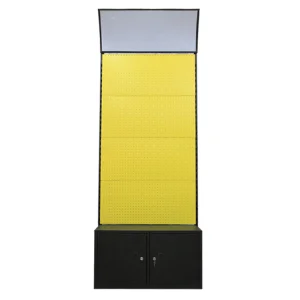
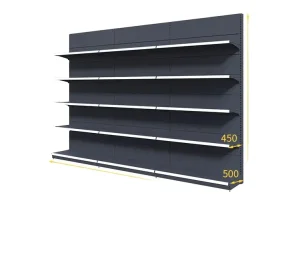
High-strength metallic pegboard display stands and industrial stacking racks designed for hanging heavy marine hardware, engine oil drums, construction fasteners, and power equipment safely.
A trusted global leader in high-density automated racking, industrial cantilever systems, and heavy-duty retail shelving solutions.
Established in 2012, Ningbo Dade Smart Storage Equipment Co., Ltd. (globally branded as DeltaStorage) operates a state-of-the-art facility spanning 48,000 square meters near Ningbo Port. Backed by 14 years of deep-rooted industry experience and 10 years of international export expertise, DeltaStorage exports over $45 million USD annually to global markets across North America, Northern Europe, East Asia, and the GCC region.
Our quality assurance infrastructure employs 82 full-time QA engineers operating within ISO14001, CE, and TUV certified frameworks. Rigorous quality control relies on spectrographic raw material alloy analysis, automated optical weld seam inspection, continuous salt-spray weathering simulation, and multi-axis dynamic load durability testing. Our R&D team of 120 experienced engineers collaborates with over 1,850 upstream and downstream supply chain partners, delivering over 120 custom product variations annually.
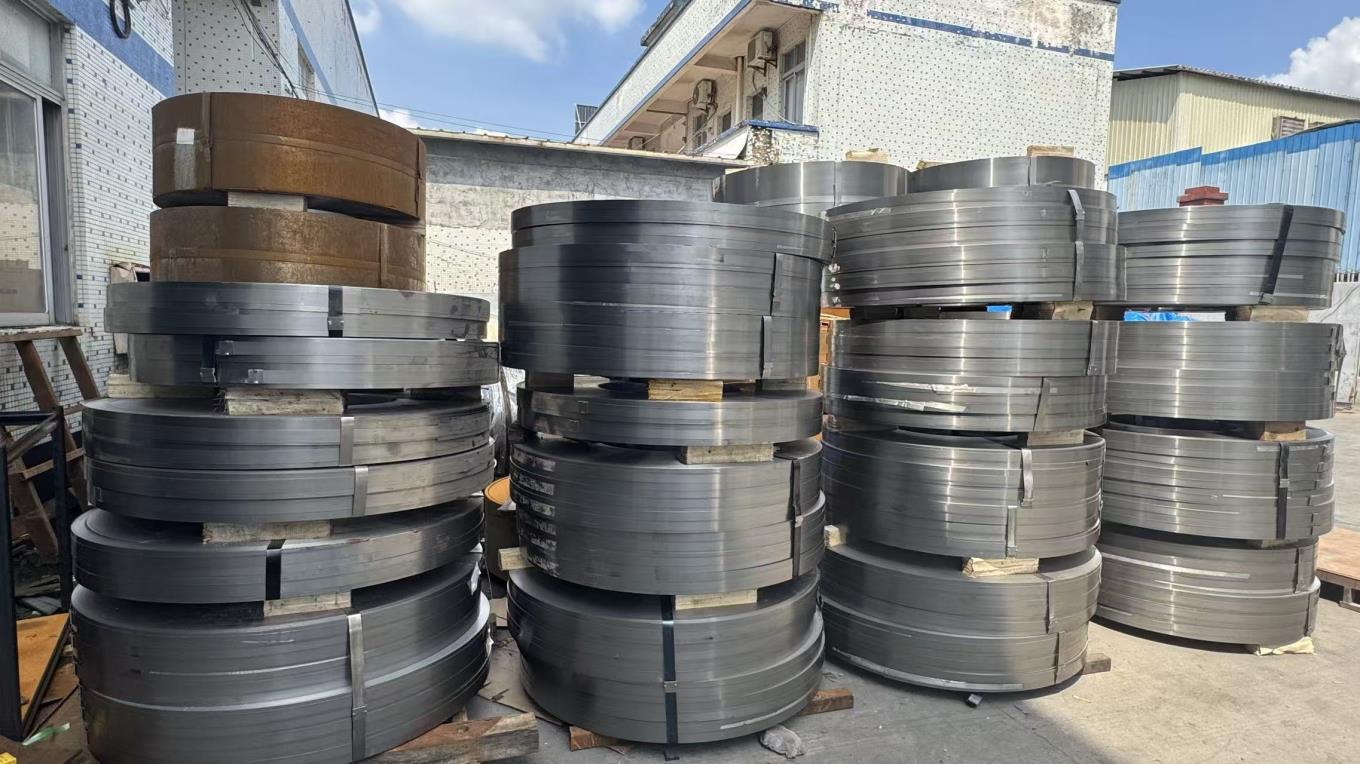
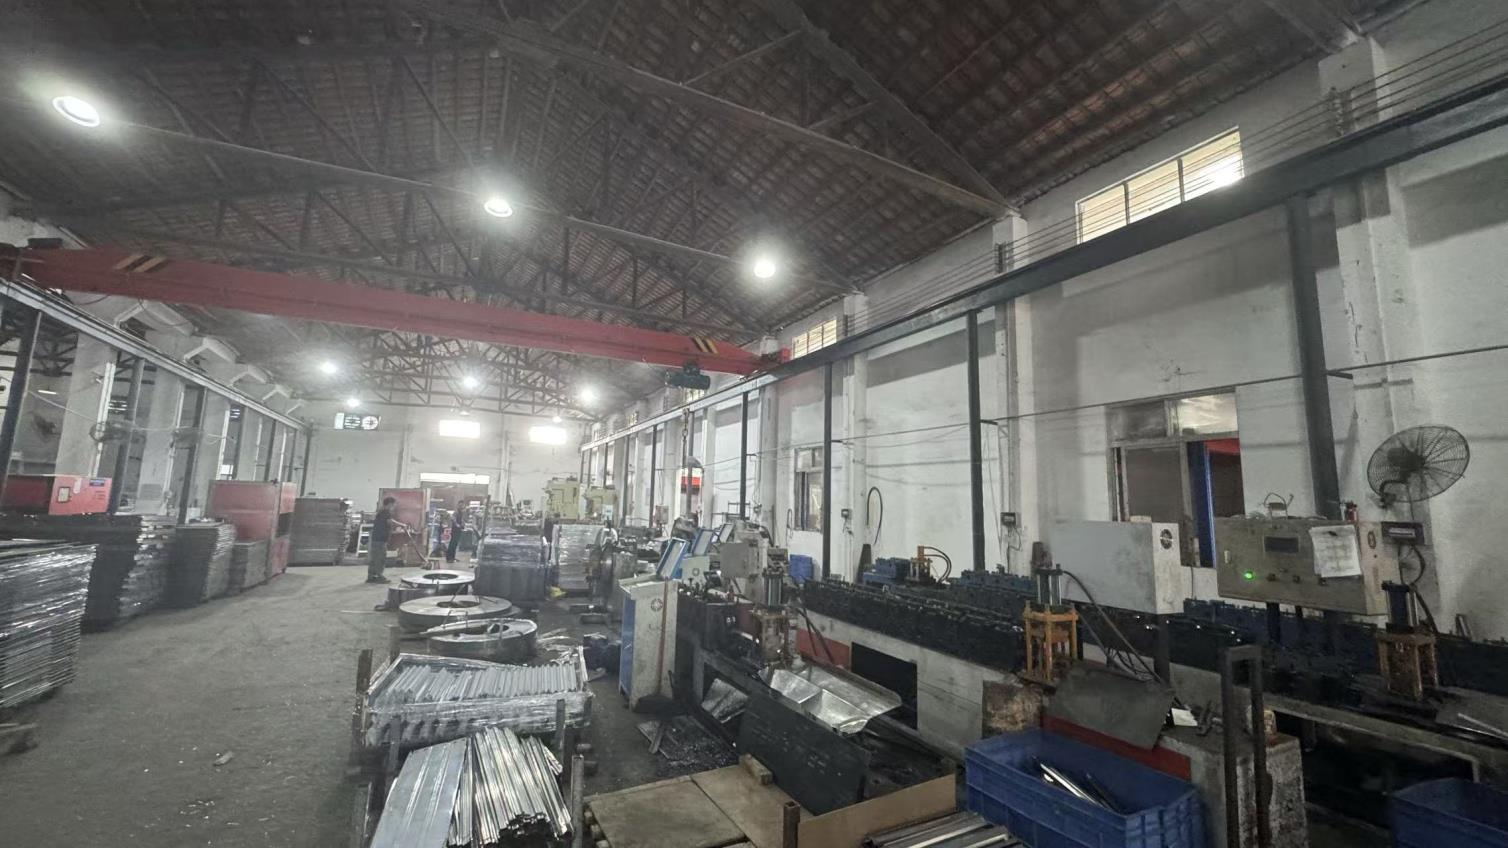
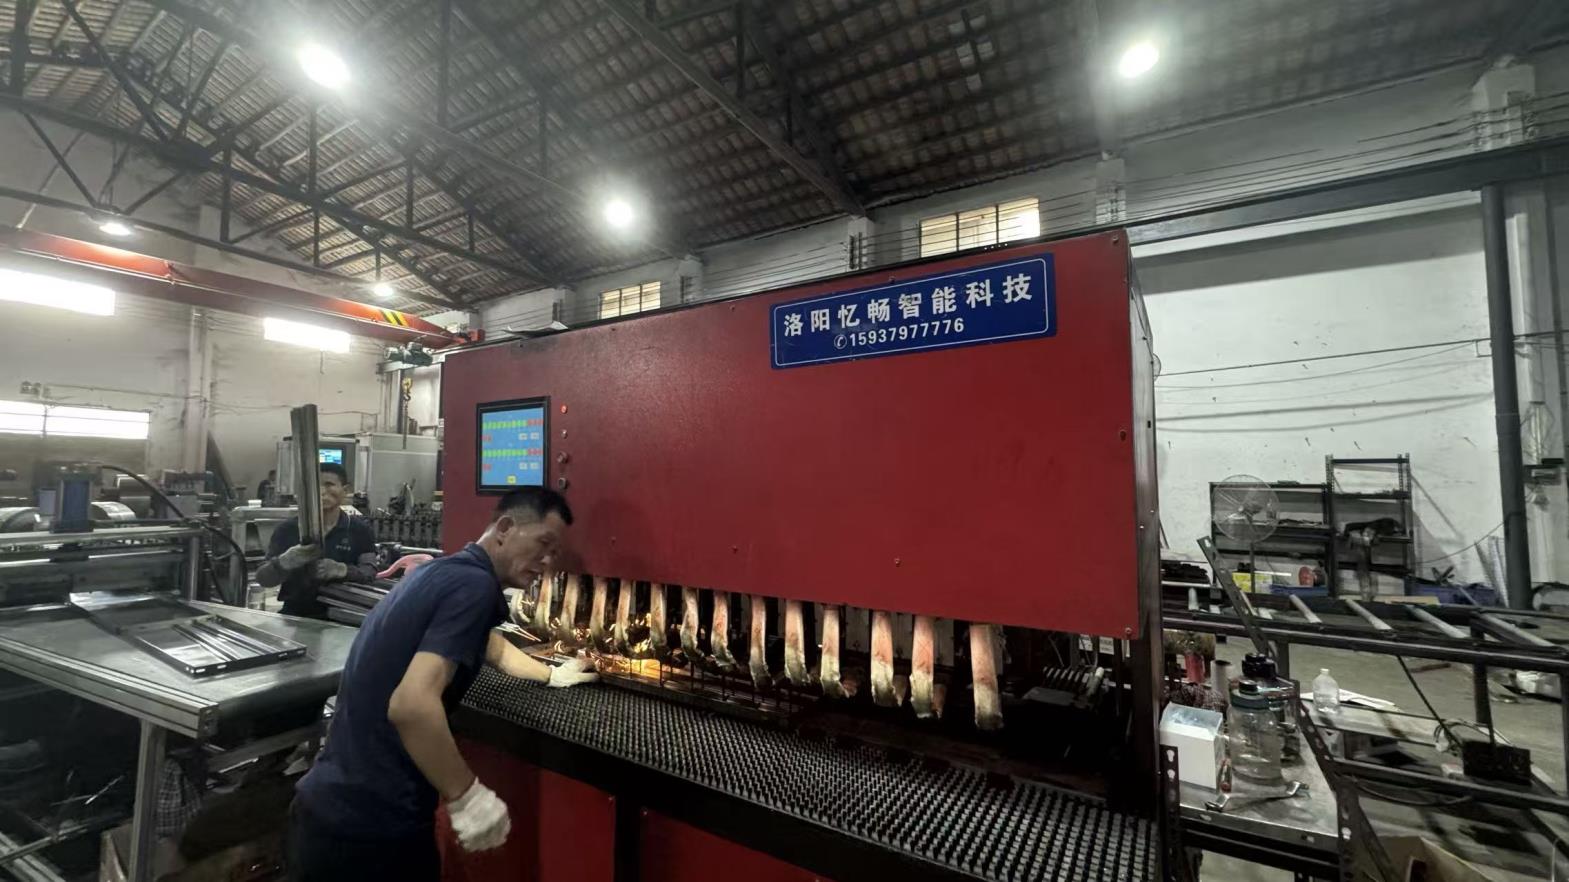
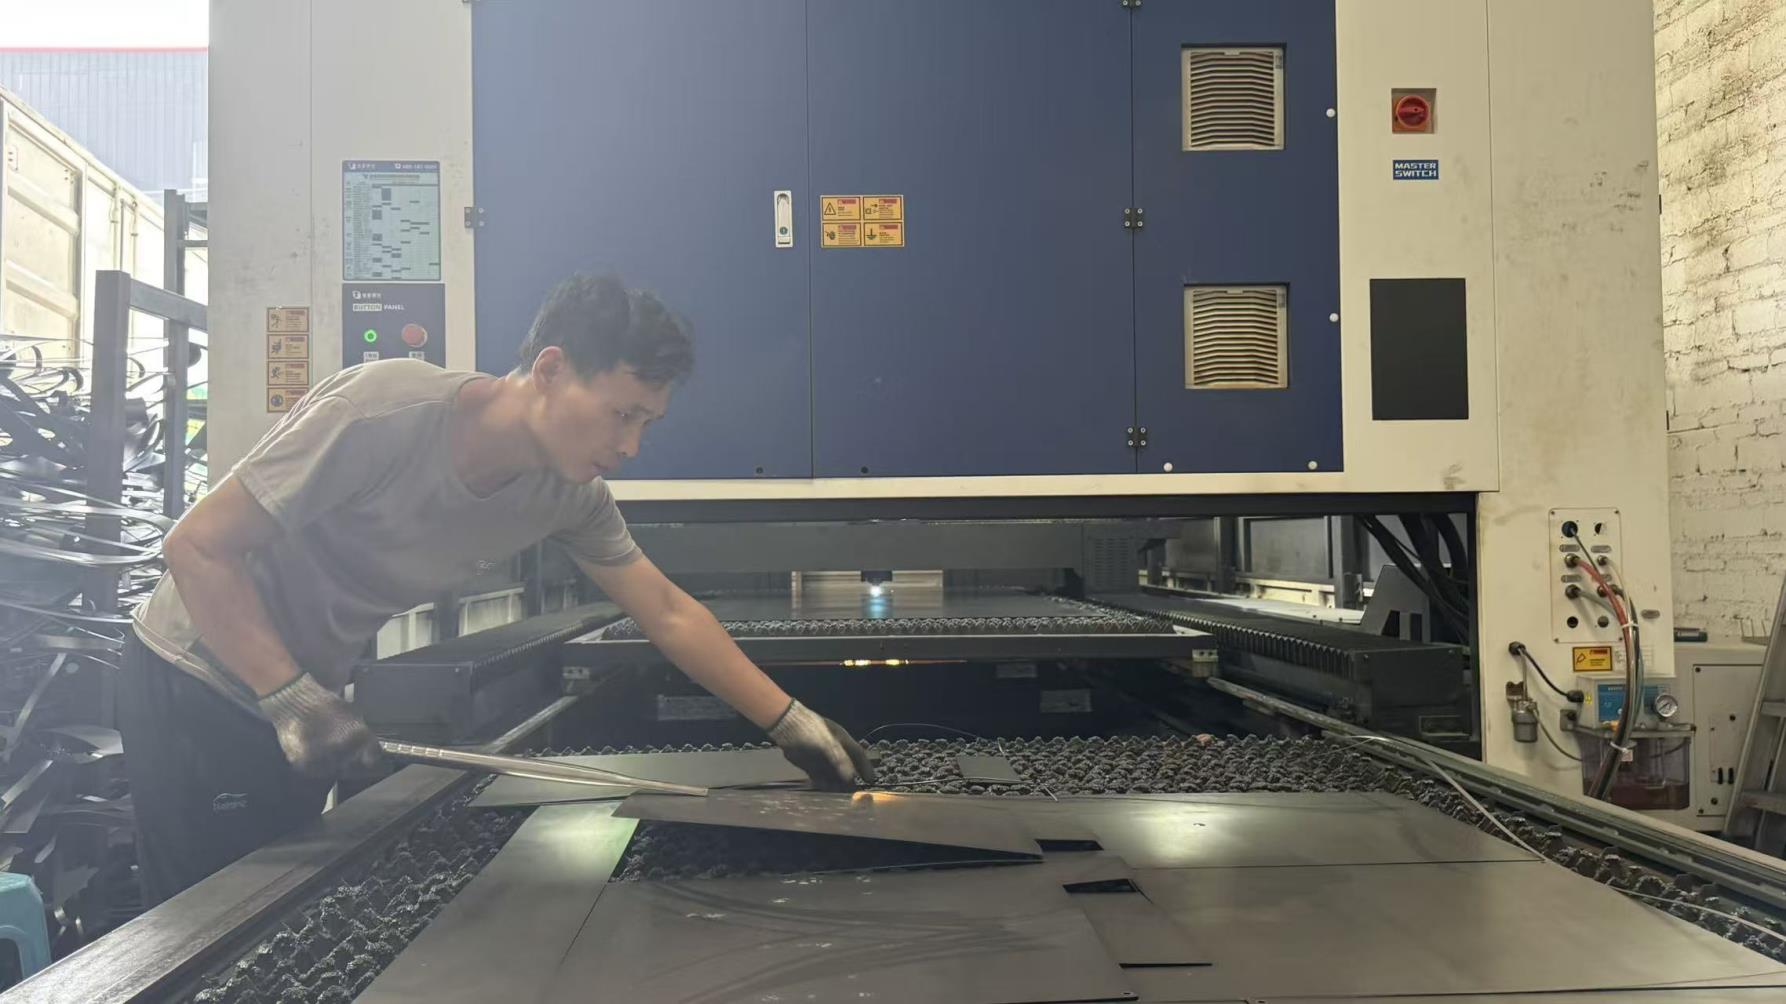
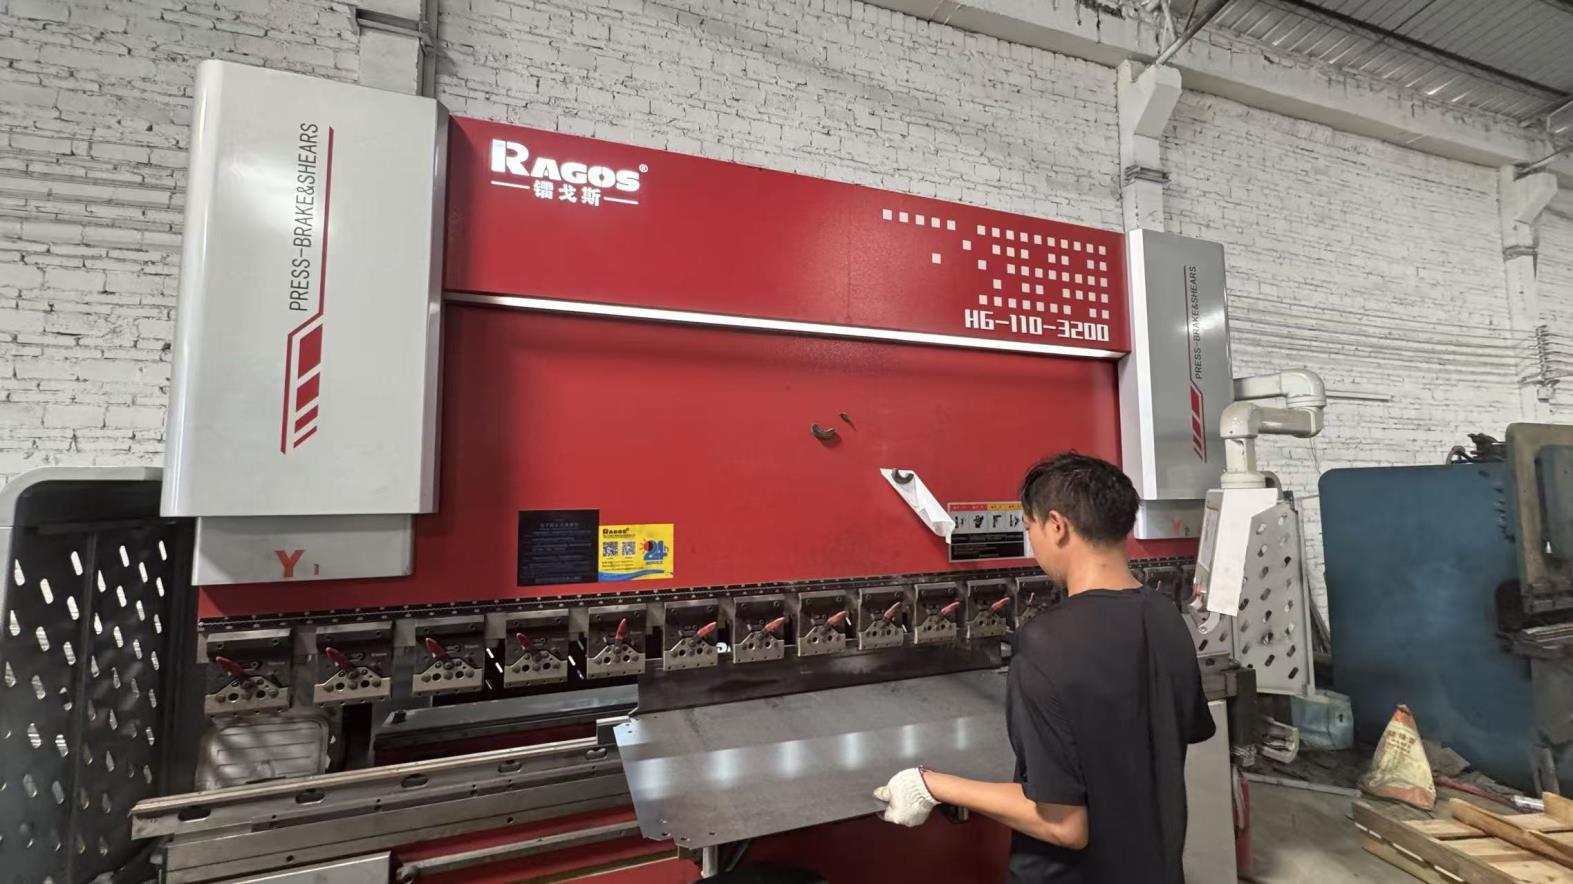
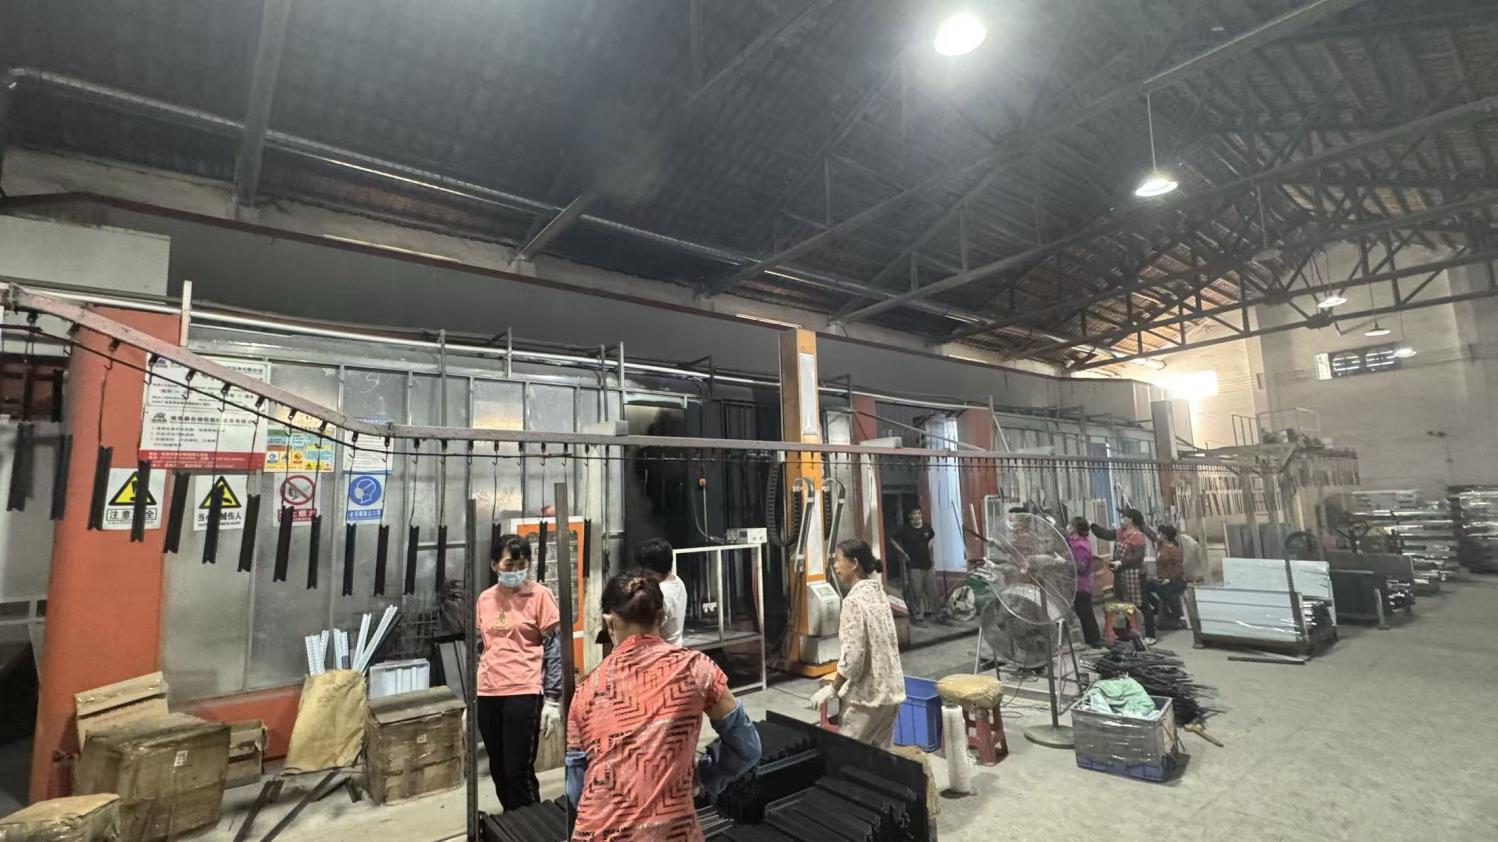
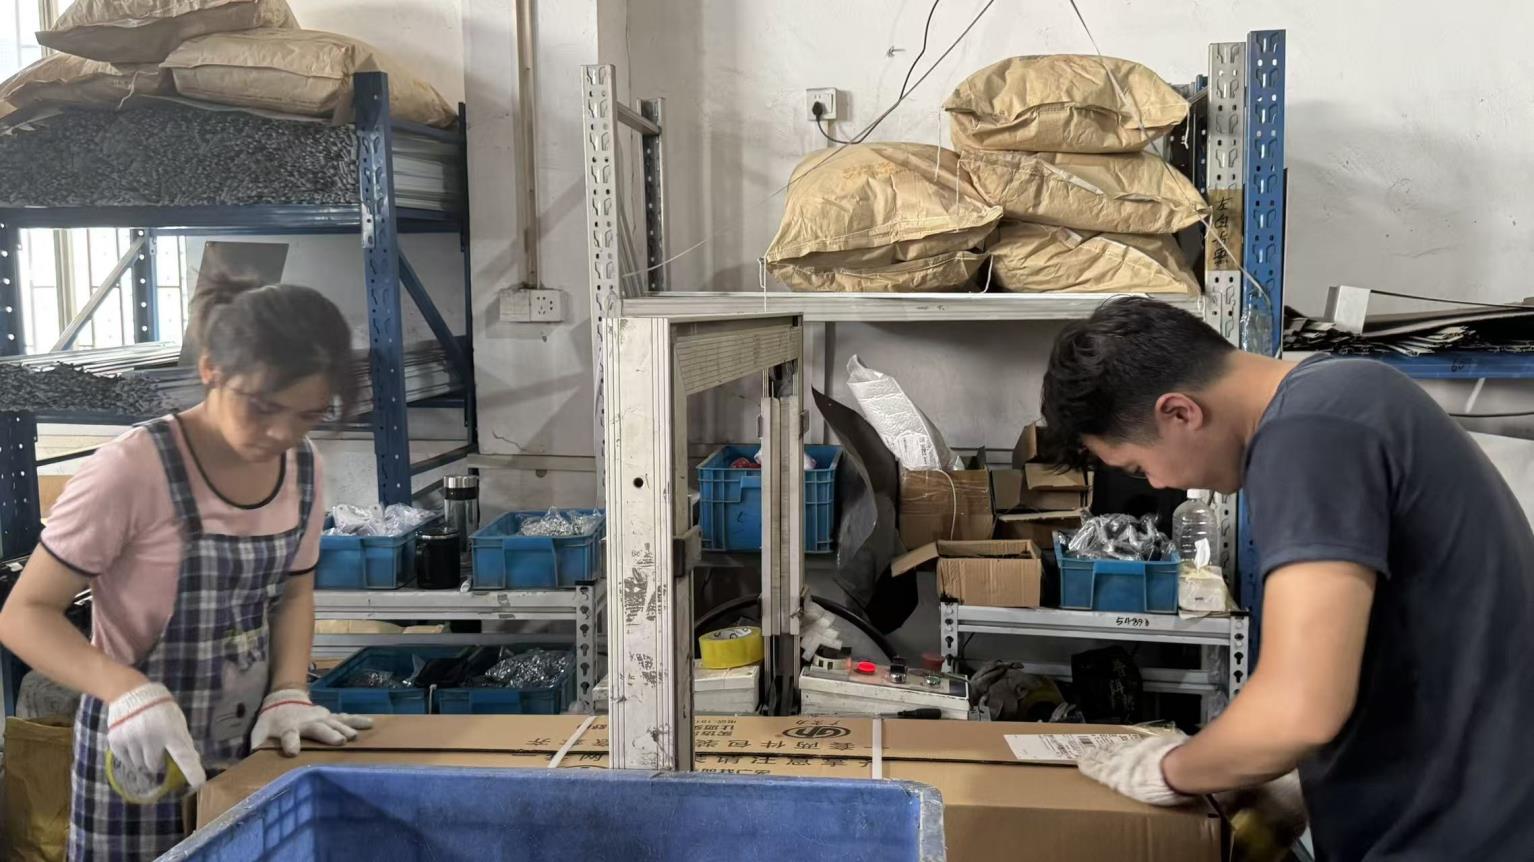
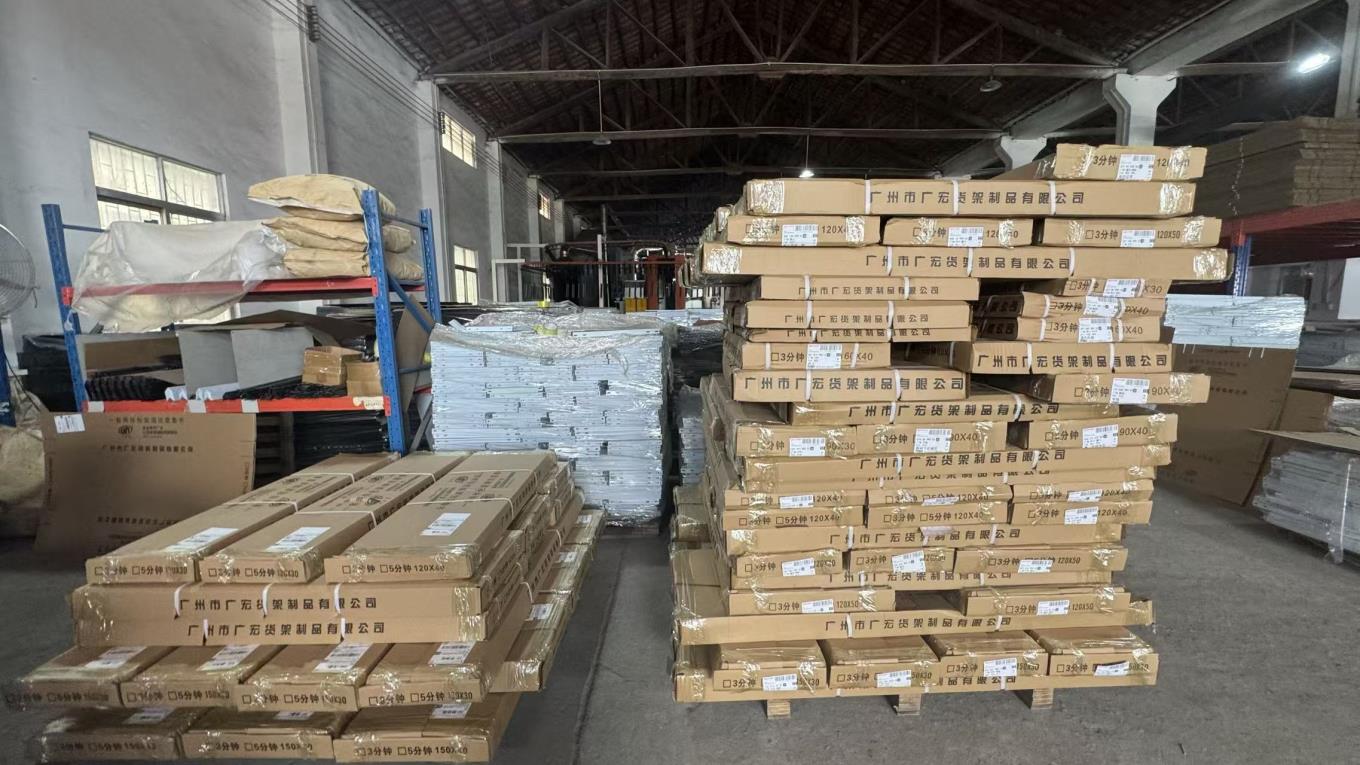
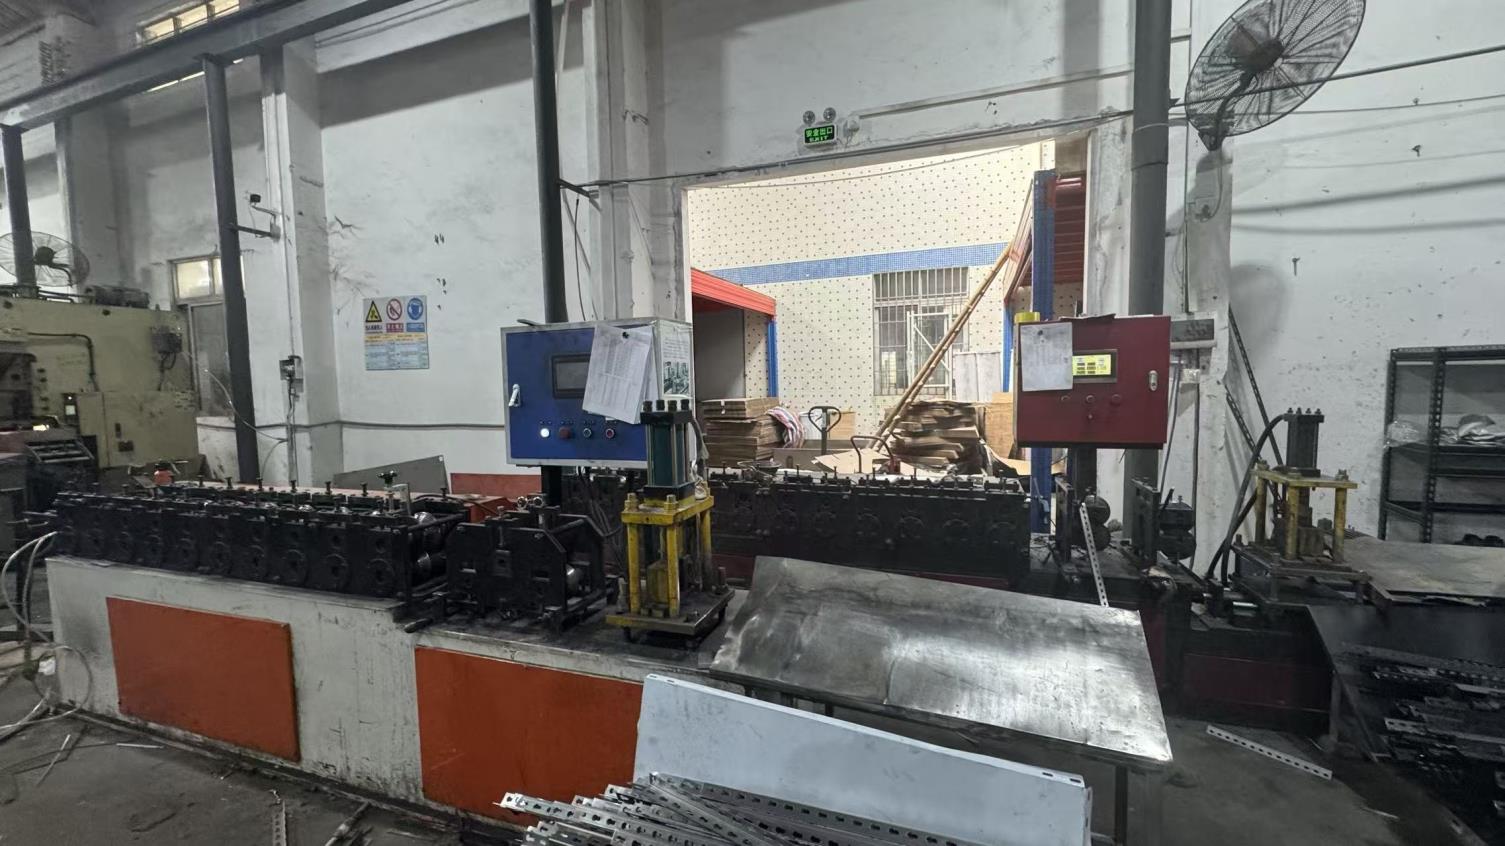
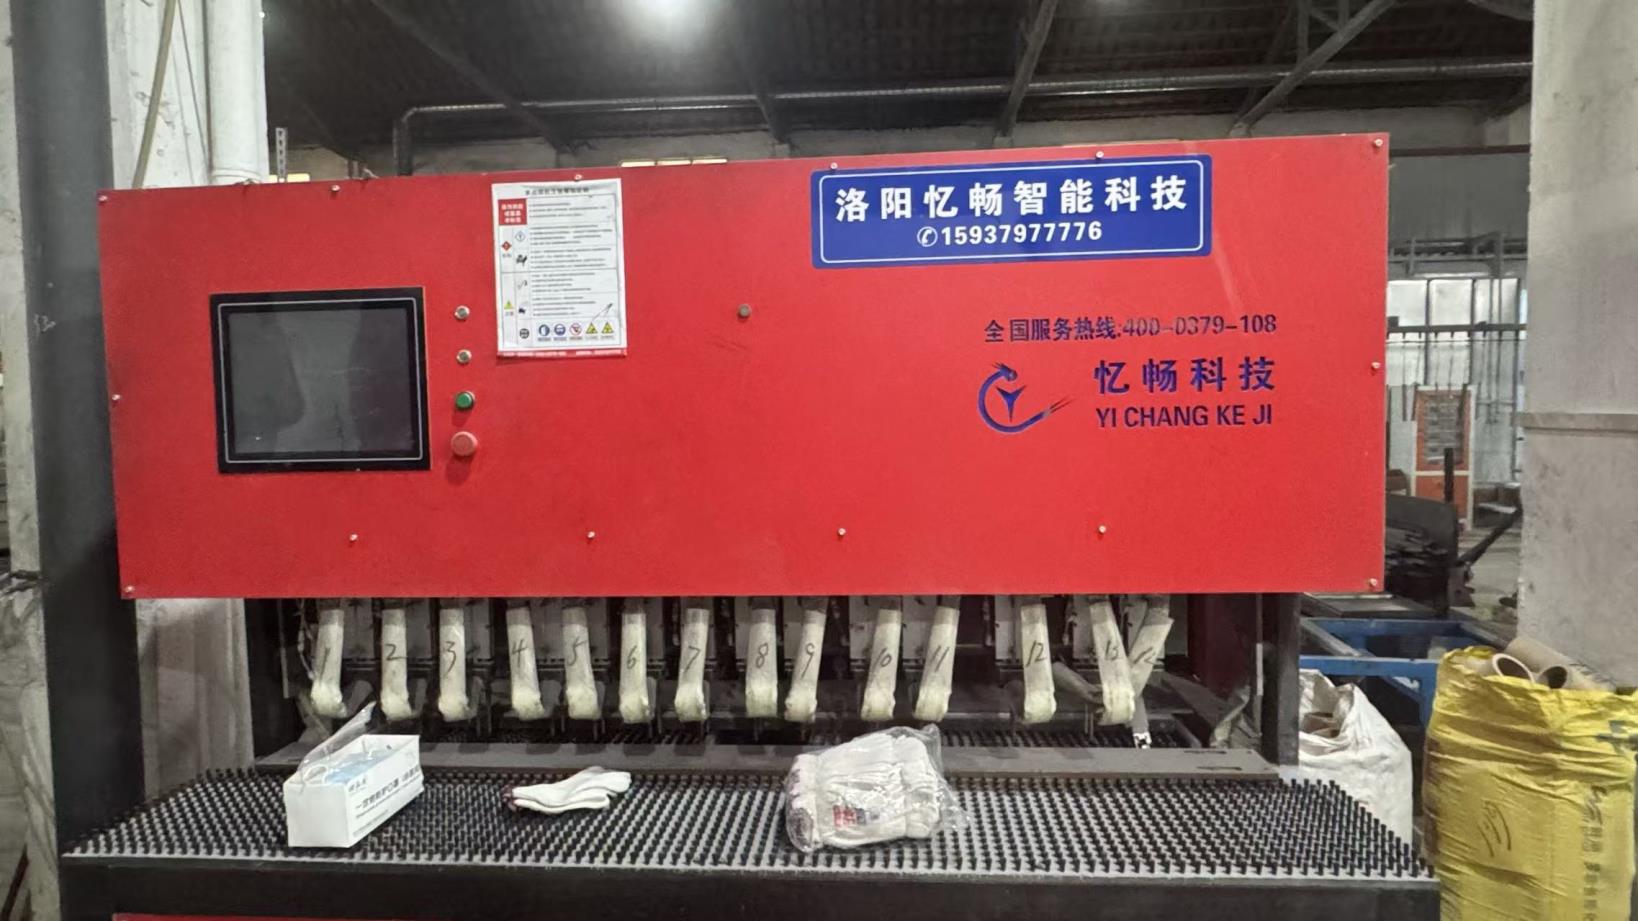
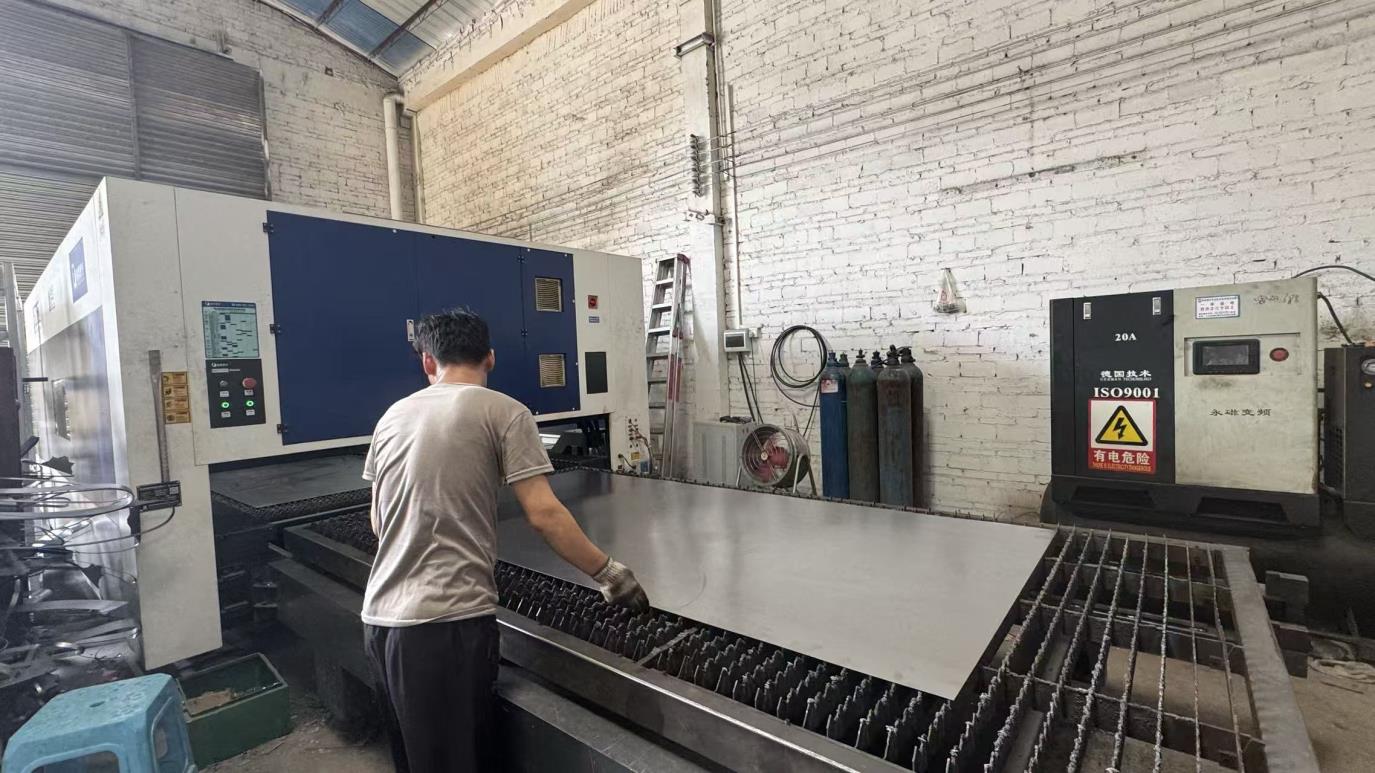
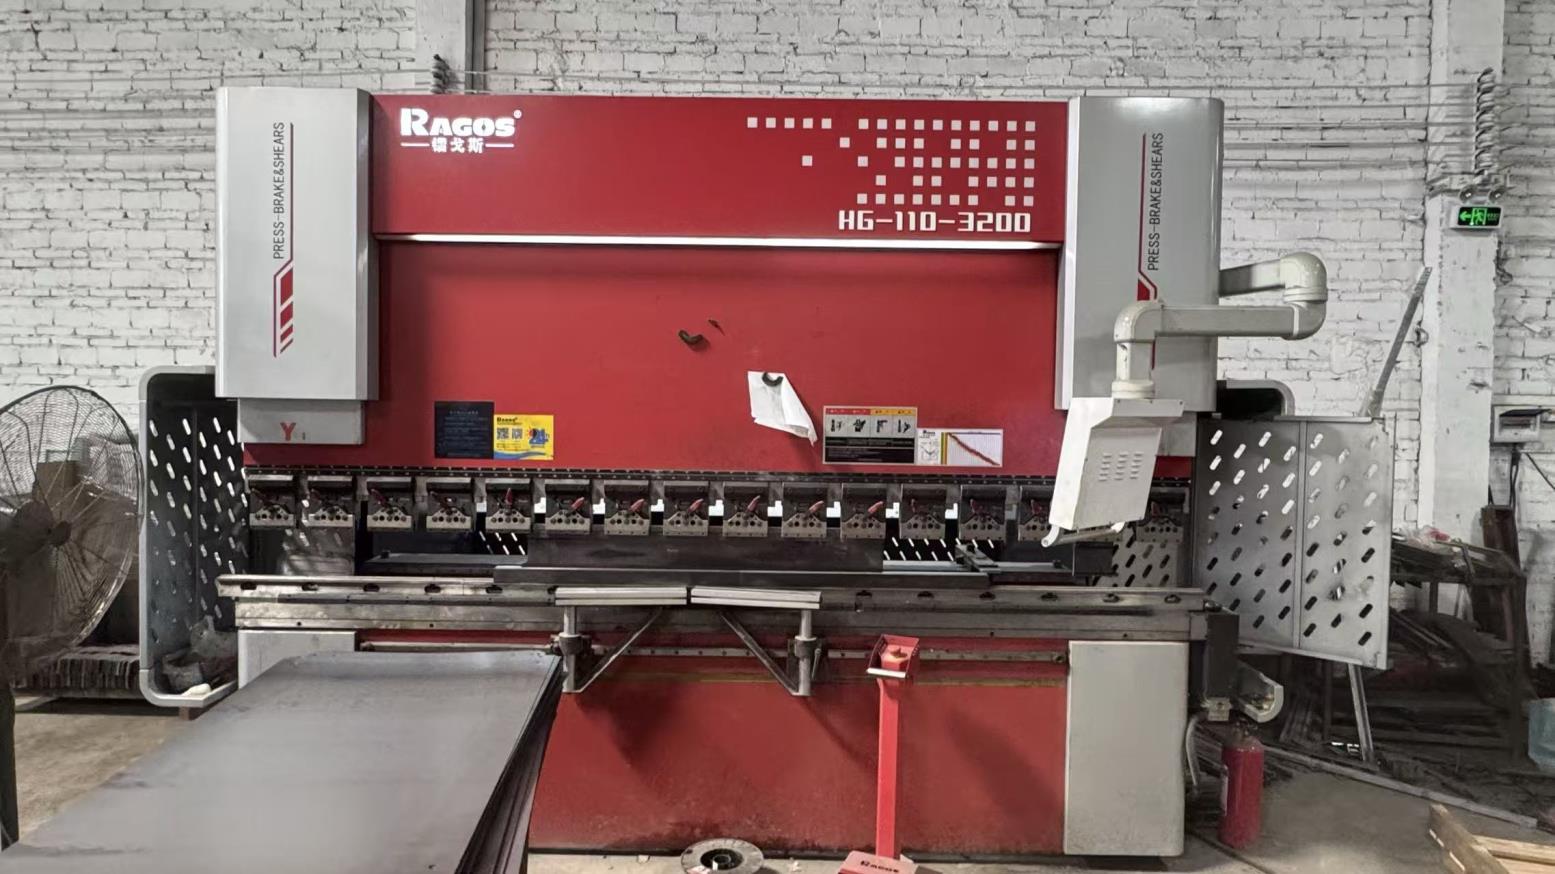
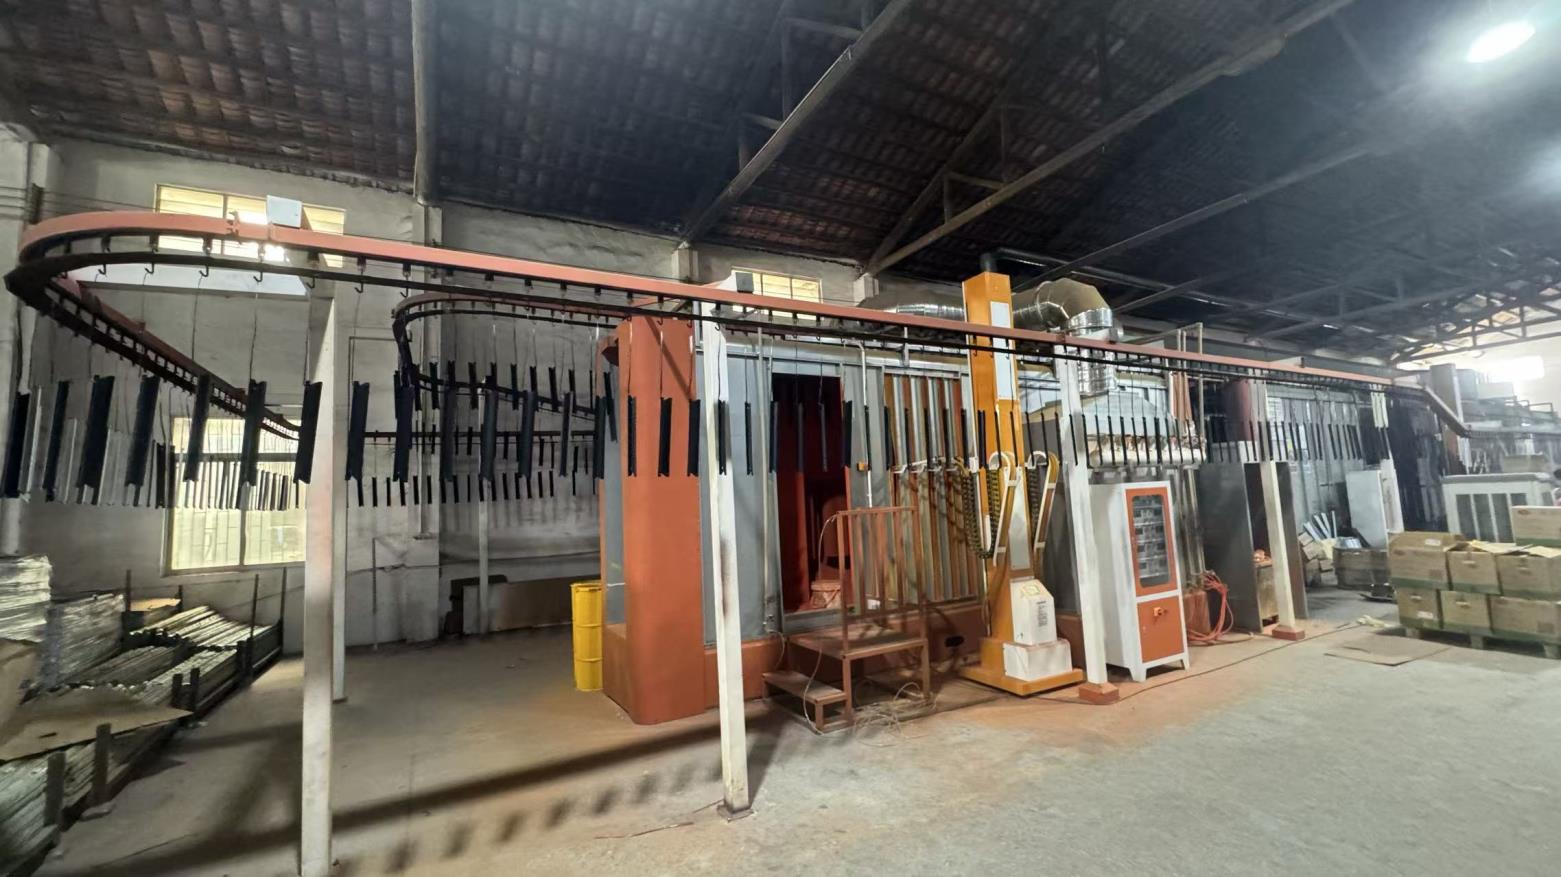
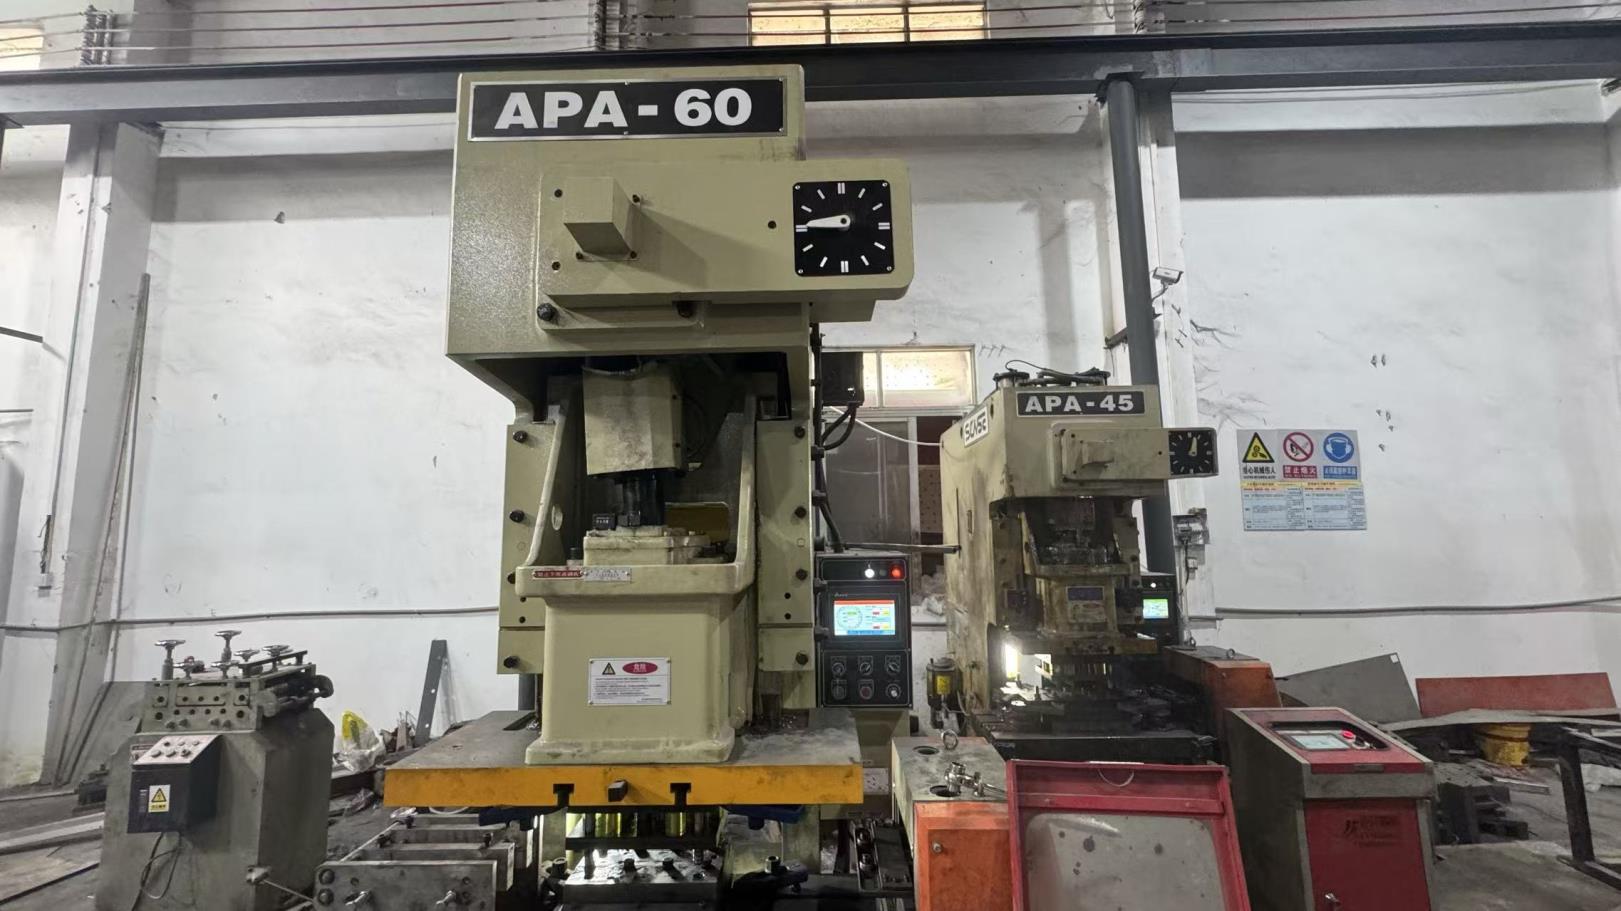
Explore our complete factory portfolio of single-sided, double-sided, pegboard, and hybrid display racks engineered for ocean freight delivery to Noro.
Expert guidance on structural parameters, ocean transport protection, and store layout optimization.
 DeltaStorage